Contract manufacturing companies comparison: Explore Key Industry Differences
Choosing a contract manufacturing partner involves more than comparing production capabilities.
Different companies can vary substantially in technical expertise, manufacturing scale, quality systems, regulatory experience, and the types of products they are equipped to handle. A useful contract manufacturing companies comparison therefore needs to look beyond a simple list of capabilities.
The contract manufacturing industry supports businesses across pharmaceuticals, medical devices, electronics, automotive components, chemicals, food production, and industrial products. As supply chains become more specialized, manufacturers increasingly need partners that can fit specific production requirements rather than simply provide general manufacturing capacity.
Understanding these differences helps organizations evaluate potential partners more systematically. The right comparison considers production processes, quality controls, engineering support, scalability, compliance, communication, and supply-chain coordination as interconnected parts of the manufacturing relationship.
Why Contract Manufacturing Companies Differ
Contract manufacturers are not interchangeable. Some specialize in high-volume standardized production, while others focus on complex, highly regulated, or technically customized products. Their facilities, equipment, workforce, certifications, and operating models are often designed around particular industries.
A manufacturer experienced in precision electronics, for example, may have sophisticated automated assembly and testing capabilities but limited experience with pharmaceutical production. Similarly, a pharmaceutical contract manufacturer may have extensive quality and regulatory systems that are irrelevant to an industrial component manufacturer.
Company size can also influence the relationship. Larger organizations may operate multiple facilities and support substantial production volumes, while specialized manufacturers may focus on narrower product categories and provide deeper technical expertise within those areas.
The comparison should therefore begin with the question of fit, rather than assuming that greater scale automatically means greater suitability.
Comparing Manufacturing Capabilities
Manufacturing capability is one of the clearest areas of differentiation. Companies may specialize in processes such as injection molding, machining, metal fabrication, electronics assembly, chemical processing, formulation, packaging, or precision assembly.
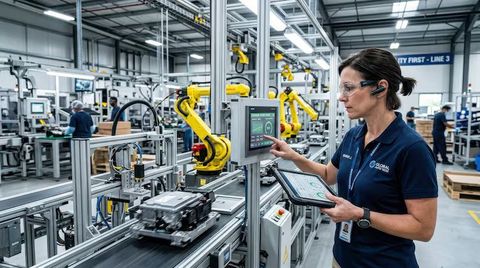
The production process required by a product determines which capabilities matter most. A manufacturer handling complex components may need advanced machining and dimensional inspection, while an electronics producer may require surface-mount technology, automated optical inspection, and functional testing.
Other factors worth examining include:
- Production equipment and technology
- Available manufacturing processes
- Prototype and pilot-production capabilities
- Quality inspection and testing infrastructure
- Automation levels
- Material-handling capabilities
- Packaging and finishing operations
A strong comparison connects these capabilities to actual product requirements. Simply counting machines or production lines does not explain whether a facility is appropriate for a particular application.
Quality Management Can Separate Similar Manufacturers
Two companies may offer similar production processes but operate very different quality systems. Quality management affects how specifications are controlled, production deviations are handled, documentation is maintained, and finished products are verified.
Depending on the industry, relevant frameworks may include ISO 9001, ISO 13485, Good Manufacturing Practice requirements, or other sector-specific standards. Regulatory expectations can be particularly demanding in pharmaceuticals, medical devices, aerospace, and other safety-sensitive industries.
Quality should therefore be evaluated throughout the manufacturing process rather than only through final inspection. Important considerations include incoming material controls, process validation, traceability, calibration, batch documentation, corrective and preventive actions, and change management.
A manufacturer with a mature quality system can provide structured evidence that production processes are controlled consistently. This becomes particularly important when products require detailed documentation or regulatory oversight.
Technology and Engineering Support
Manufacturing is increasingly connected to engineering. Product designs may need modification for manufacturability, material selection, tolerance optimization, automation, or production efficiency.
Some contract manufacturing companies primarily execute established production specifications. Others maintain engineering teams capable of working with customers during product development and process improvement.
This distinction can significantly affect the manufacturing relationship.
Engineering support may include:
- Design-for-manufacturing analysis
- Process development
- Tooling and fixture development
- Material evaluation
- Prototype support
- Production testing
- Process optimization
A company developing a new product may need more engineering involvement than an organization transferring an established design into an existing production environment.
Production Scale and Scalability
Manufacturing requirements can change significantly over a product's lifecycle. Early production may involve relatively small quantities, while successful products can eventually require much larger output.
This makes scalability an important comparison factor.
A manufacturer should be evaluated on whether it can support the transition between production stages without creating unnecessary disruption. Relevant considerations include available floor space, equipment capacity, workforce flexibility, supplier relationships, production planning, and the ability to add shifts or manufacturing resources.
However, larger capacity is not automatically advantageous. Excess capacity does not compensate for weak technical compatibility or inadequate quality controls. The useful question is whether the company's capacity aligns with the expected production pattern.
Regulatory and Industry Experience
Regulatory knowledge becomes increasingly important as manufacturing moves into specialized industries. Requirements can influence facility design, documentation, validation, testing, material control, labeling, and production records.
In regulated manufacturing, experience with the relevant regulatory environment can reduce the risk of misunderstandings during production and quality reviews.
Industry experience also provides practical knowledge that may not appear in a capability brochure. A manufacturer familiar with a particular product category may already understand common material issues, testing requirements, process constraints, and documentation expectations.
For this reason, experience should be evaluated in relation to the specific product and industry rather than measured only by the number of years a company has operated.
Supply Chain and Production Coordination
Contract manufacturing rarely involves production in isolation. Materials, components, packaging, logistics, inventory, forecasting, and production scheduling all influence manufacturing performance.
Some manufacturers provide extensive supply-chain coordination, while others operate mainly as production facilities and expect customers to manage upstream materials.
This difference can affect operational complexity.
A broader manufacturing relationship may involve:
- Supplier coordination and material planning
- Incoming material inspection
- Production scheduling
- Inventory management
- Assembly and testing
- Packaging and documentation
- Shipment coordination
The appropriate model depends on how much operational responsibility an organization wants its manufacturing partner to manage.
Comparing Communication and Operational Transparency
Technical capability is only one part of a successful manufacturing relationship. Communication becomes especially important when specifications change, production issues occur, materials are delayed, or schedules need adjustment.
A contract manufacturer should have clear processes for reporting production status, quality issues, engineering changes, and supply-chain disruptions.
Change control deserves particular attention. Even a seemingly minor modification to a material, component, process, or production location can affect product performance or regulatory documentation.
Companies with disciplined communication and change-management procedures can make these transitions easier to track and evaluate.
A Practical Comparison Framework
A useful contract manufacturing companies comparison can be organized around several major dimensions:
| Comparison Area | What to Examine |
|---|---|
| Manufacturing capability | Processes, equipment, materials, production methods |
| Quality management | Quality systems, inspection, traceability, corrective actions |
| Engineering | Design support, process development, tooling, testing |
| Scale | Capacity, production flexibility, expansion capability |
| Regulatory experience | Applicable standards, documentation, validation |
| Supply chain | Materials, inventory, suppliers, logistics coordination |
| Technology | Automation, monitoring, testing, manufacturing systems |
| Communication | Reporting, escalation, change management |
| Product experience | Relevant industry and process knowledge |
This framework is more useful than comparing companies by size alone because it connects organizational capabilities to actual manufacturing requirements.
How Manufacturing Priorities Change by Industry
The most important comparison criteria can vary considerably between industries.
Pharmaceutical manufacturing places strong emphasis on process control, documentation, validation, contamination controls, and regulatory compliance. Medical device manufacturing may place additional emphasis on design controls, traceability, quality systems, and product verification.
Electronics manufacturing often requires precision assembly, automated inspection, component management, and functional testing. Industrial manufacturing may place greater emphasis on machining accuracy, material properties, durability testing, and production engineering.
These differences demonstrate why there is no universal definition of an appropriate contract manufacturer. The evaluation must reflect the product's technical, regulatory, and operational environment.
Questions to Consider Before Selecting a Manufacturer
A structured evaluation can help identify important differences before a manufacturing relationship begins. Useful questions include:
- Does the manufacturer have experience with the required production process?
- Can its quality system support the product's regulatory requirements?
- Can production capacity accommodate expected changes in volume?
- What engineering resources are available?
- How are design and process changes controlled?
- How are materials and suppliers managed?
- What testing and inspection capabilities are available?
- How are production issues communicated and escalated?
The answers should be supported by documented capabilities and established processes rather than general claims.
Conclusion
A meaningful contract manufacturing companies comparison looks at much more than production capacity. Manufacturing processes, quality systems, engineering resources, regulatory experience, scalability, supply-chain coordination, and communication can all influence how effectively a company fits a particular production requirement.
The strongest evaluation is therefore product-specific and evidence-based. By comparing manufacturers across the capabilities that actually matter to the product and its lifecycle, organizations can develop a clearer understanding of operational fit and make more informed manufacturing decisions.