Industrial Robotic Palletizers Information With Automated Palletizing and Handling Systems
Industrial robotic palletizers are automated machines designed to arrange boxes, bags, cartons, cases, trays, containers, or other packaged products onto pallets. They combine robotic arms, grippers, conveyors, sensors, control systems, and pallet-handling equipment to create organized load patterns for storage and transportation.
Automated palletizing has become an important part of industrial material handling because packaged products often need to be moved repeatedly between production, warehousing, and distribution areas.
Traditional palletizing relied heavily on manual placement. Workers positioned individual packages on pallets according to a planned pattern, with the process repeated for large numbers of products. As manufacturing and packaging operations became more automated, robotic palletizers developed as a way to connect packaging lines with downstream material-handling systems.
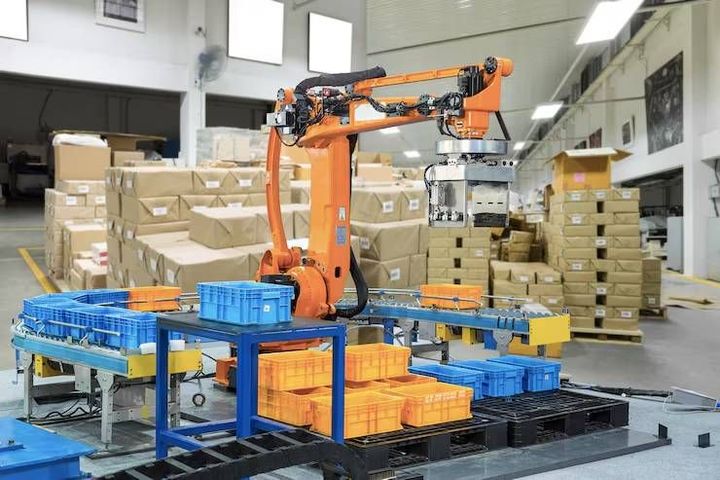
A robotic palletizing system normally begins with products arriving on a conveyor. Sensors and control software identify the products and coordinate their movement toward the robotic cell. A robotic arm then picks up one or more packages and places them onto a pallet according to a programmed arrangement.
The system may also include pallet dispensers, pallet conveyors, safety fencing, machine-vision equipment, automatic layer formation, slip-sheet handling, and stretch-wrapping equipment. The exact configuration depends on product dimensions, package weight, pallet size, production speed, and the required handling sequence.
Main Components of Robotic Palletizers
An automated palletizing cell can contain several interconnected components:
Robotic arm for package movement
End-of-arm tooling for gripping products
Product conveyors for controlled movement
Sensors for package detection and positioning
Pallet conveyors for pallet movement
Pallet dispensers for automatic pallet positioning
Controllers for coordinating equipment
Human-machine interfaces for operator interaction
Safety scanners, guards, and interlocks
Vision systems for selected identification and positioning tasks
The end-of-arm tooling is particularly important because different products require different gripping methods. Vacuum grippers may be appropriate for certain packaging formats, while mechanical clamps or specialized gripping devices may be used for other products.
Importance
Industrial robotic palletizers are important because palletizing is a repetitive material-handling activity found in many manufacturing and packaging environments. Automating this stage can connect packaging lines with warehouse handling while reducing the amount of repetitive manual movement required.
Robotic palletizing also helps establish consistent package arrangements. A programmed pattern can determine how products are positioned within each layer and how multiple layers are stacked on a pallet.
Industries Using Robotic Palletizers
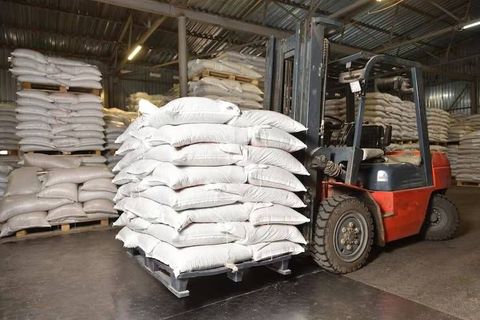
Robotic palletizing systems are used across many industrial sectors. Applications can include food and beverage packaging, consumer goods, chemicals, building materials, paper products, agricultural products, household products, and industrial components.
The system configuration changes according to the product. Lightweight cartons may require different gripping equipment from heavy bags, while irregular containers may require vision systems or customized tooling.
Production and Material Flow
A robotic palletizer generally forms part of a larger production line rather than operating independently. Products can arrive from filling, packaging, labeling, or inspection equipment before reaching the palletizing cell.
A typical material flow may include:
Product packaging
Conveyor transfer
Product detection
Product grouping
Robotic picking
Layer formation
Pallet placement
Layer completion
Pallet transfer
Wrapping or stabilization
Warehouse movement
The arrangement should allow sufficient space around conveyors, robotic movement, pallet storage, and maintenance areas. Pallet movement also needs to be coordinated with forklifts, automated guided vehicles, or other warehouse equipment where applicable.
Workplace Considerations
Robotic palletizers contain moving arms and automated equipment that can create hazards when people enter operating areas unexpectedly. Safety systems therefore form an important part of robotic palletizing design.
Depending on the equipment, protection can include physical guarding, safety scanners, interlocked gates, emergency-stop controls, light curtains, warning systems, and controlled access zones. Operators also need appropriate procedures for setup, inspection, cleaning, troubleshooting, and maintenance.
Recent Updates
Industrial robotic palletizing has continued to develop through improvements in robotic control, machine vision, end-of-arm tooling, digital monitoring, and integration with wider production systems. Current systems increasingly combine physical automation with software that manages product patterns and operating information.
Flexible Palletizing
Modern robotic palletizers can be configured to handle multiple package sizes and pallet patterns. Software can store different recipes or programs so that the system can change between defined production configurations.
This flexibility is particularly relevant where facilities process several product formats. Instead of requiring an entirely separate arrangement for every package type, a suitably configured robotic cell can accommodate multiple operating sequences.
Vision and Sensing
Machine-vision technology can provide information about package position, orientation, shape, or identification. Cameras and sensors can help the control system determine whether products are correctly positioned before robotic handling.
Vision technology can be particularly useful when products do not always arrive in exactly the same position. The system can use detected information to adjust robotic movement within the limits of its programmed operation.
Collaborative Automation
Some industrial environments are exploring collaborative robotic technologies for selected handling applications. These systems are designed with specific safety functions that can support controlled interaction between people and robotic equipment.
Collaborative operation does not mean that every robotic application can operate without guarding. A risk assessment remains important because product weight, robot movement, tooling, speed, and surrounding machinery all influence the safety requirements.
Digital Monitoring
Connected robotic palletizers can collect information about cycle counts, equipment status, alarms, operating patterns, and production activity. Digital dashboards can display selected information to operators and maintenance teams.
Integration with manufacturing execution systems and warehouse platforms can also connect palletizing information with wider production and inventory processes. Communication between systems needs to be planned around compatible industrial protocols and data structures.
Advanced End-of-Arm Tooling
Gripper technology continues to evolve for different package shapes and materials. Vacuum systems, mechanical grippers, multi-product tooling, and adaptive mechanisms can be configured for particular applications.
Tooling selection affects the robot's payload, movement characteristics, package stability, and operating sequence. It is therefore an important part of robotic palletizer design.
Laws or Policies
Industrial robotic palletizers are affected by machinery safety, workplace protection, electrical safety, building requirements, and industrial automation standards. The applicable rules depend on the country, facility, equipment configuration, and industry.
Machinery Safety
Robotic palletizing cells generally require measures to control access to moving equipment. Safety systems may include protective barriers, interlocked doors, emergency stops, safety-rated monitoring devices, and controlled operating modes.
Risk assessment is an important part of machine integration. Designers and facility operators need to consider robot movement, gripper behavior, pallet movement, falling products, unexpected restarts, and maintenance activities.
Electrical and Control Requirements
Robotic palletizers include motors, controllers, sensors, drives, electrical panels, and communication equipment. Electrical installation requirements can address grounding, protection against electrical hazards, control-panel construction, wiring, and emergency systems.
Automated systems may also need documentation covering control architecture, operating modes, safety circuits, and maintenance procedures.
Workplace Safety
Workers who interact with robotic palletizers may need training related to normal operation, access restrictions, emergency procedures, equipment isolation, and maintenance. Lockout or energy-isolation procedures can be relevant when workers need to enter areas containing hazardous mechanical, electrical, pneumatic, or hydraulic energy.
Regulatory requirements differ between jurisdictions, so facility-specific assessments are necessary to determine which rules apply.
Tools and Resources
Planning an industrial robotic palletizer involves mechanical, electrical, software, and facility-layout information. Robot simulation software can help visualize arm movement, pallet patterns, reach distances, cycle sequences, and potential interference between components.
Pallet pattern software can be used to calculate how packages can be arranged on different pallet sizes. This can help planners examine layer configurations before programming the physical robot.
Useful resources include:
Robot specification sheets
End-of-arm tooling specifications
Pallet pattern calculators
Robot simulation platforms
Conveyor layout drawings
Production flow diagrams
Safety risk assessment templates
Preventive maintenance schedules
Robot programming documentation
Equipment inspection checklists
Manufacturing execution platforms
Warehouse management systems
A simplified comparison of robotic palletizer configurations is shown below:
| Palletizer Configuration | Typical Application | Main Planning Factor |
|---|---|---|
| Single-Robot Cell | One product flow | Robot reach |
| Multi-Product Cell | Several package formats | Tooling flexibility |
| High-Speed Palletizer | Continuous production | Conveyor synchronization |
| Bag Palletizer | Flexible or filled bags | Gripper design |
| Case Palletizer | Cartons and cases | Package dimensions |
| Layer Palletizer | Grouped product layers | Layer formation |
| Integrated Pallet Cell | Multiple automated stages | System coordination |
Facility-layout software can also help determine robot reach, pallet locations, operator pathways, conveyor positions, and maintenance clearances. Digital simulation can provide a visual representation of the proposed cell before equipment installation.
FAQs
What are industrial robotic palletizers?
Industrial robotic palletizers are automated robotic systems that arrange packaged products onto pallets. They typically combine robotic arms, grippers, conveyors, sensors, controllers, and pallet-handling equipment.
How do automated palletizing systems work?
Products arrive through a conveyor and are detected by sensors or vision equipment. The robotic arm picks up products using specialized tooling and places them onto a pallet according to a programmed pattern.
What products can industrial robotic palletizers handle?
Robotic palletizers can be configured for cartons, cases, bags, trays, containers, boxes, and other packaged products. The suitable configuration depends on product dimensions, weight, shape, packaging material, and required pallet pattern.
What are the main benefits of automated palletizing?
Automated palletizing can reduce repetitive manual handling, maintain programmed stacking patterns, coordinate product movement, and connect packaging operations with warehouse processes. The actual results depend on system design and operating conditions.
What factors should be considered when planning a robotic palletizer?
Important factors include product dimensions, package weight, production flow, robot reach, payload, gripper design, pallet dimensions, conveyor arrangement, safety systems, floor space, maintenance access, and integration with other automation equipment.
Conclusion
Industrial robotic palletizers combine robotic arms, gripping equipment, conveyors, sensors, controllers, and pallet-handling systems to automate repetitive product stacking activities. Recent developments include flexible pallet patterns, machine vision, advanced tooling, digital monitoring, and integration with broader manufacturing systems. Safe operation depends on appropriate guarding, controls, risk assessment, operator procedures, and applicable machinery requirements. The final system configuration varies according to product characteristics, production flow, pallet format, facility layout, and automation architecture.