Chemical Raw Material Suppliers Overview With Quality, Applications, and Procurement Information
Chemical raw material suppliers play an important role in manufacturing, industrial processing, agriculture, construction, textiles, packaging, and many other industries. They connect chemical producers with businesses that require specific substances to manufacture finished goods.
These materials may include solvents, acids, alkalis, resins, pigments, additives, industrial salts, and specialty compounds used in different production processes.
Chemical raw materials originate from various sources, including petroleum processing, mineral extraction, natural gas processing, agricultural resources, and industrial chemical synthesis. Their properties depend on their composition, manufacturing method, concentration, and intended application. Some materials serve as primary ingredients, while others support cleaning, surface treatment, temperature control, or product formulation.
Chemical raw material suppliers help organize the movement of these substances from manufacturers to industrial users. Their activities may include sourcing, packaging, storage, transportation coordination, documentation, and product quality verification. The specific responsibilities vary according to the supplier's business model and the chemical category involved.
Understanding chemical raw material suppliers is useful for manufacturers, procurement teams, laboratory personnel, and people researching industrial production. Knowledge of material specifications, supplier qualifications, handling requirements, and procurement procedures helps explain how chemical inputs move through modern supply chains.
Common Types of Chemical Raw Materials
Chemical materials differ according to their composition and intended use. Common categories include:
Organic chemicals, including selected alcohols, solvents, and organic acids used in manufacturing.
Inorganic chemicals, such as mineral-based compounds, industrial salts, acids, and alkalis.
Polymers and resins, which support plastics manufacturing, coatings, adhesives, and composite production.
Pigments and additives, which influence color, stability, texture, and processing characteristics.
Specialty chemicals, which are formulated for particular industrial functions or technical requirements.
Each category requires different specifications, storage conditions, and handling procedures. A material suitable for one manufacturing process may be unsuitable for another, even when the chemical names appear similar.
How the Supply Chain Works
The chemical supply chain generally begins with a producer or chemical processing facility. Materials then move through distributors, wholesalers, storage facilities, or specialist suppliers before reaching industrial users.
During this process, packaging integrity, batch identification, transport conditions, and documentation help maintain material traceability. Depending on the product, buyers may receive technical data sheets, safety data sheets, certificates of analysis, and information about concentration or purity.
Importance
Chemical raw material suppliers matter because industrial production depends on consistent access to inputs with suitable chemical and physical properties. A shortage, delayed shipment, or specification mismatch can interrupt manufacturing schedules, affect product quality, and create additional handling requirements.
Their importance extends beyond factories. Chemical inputs contribute to products used in buildings, household cleaning, food packaging, clothing, electronics, water treatment, and transportation. Reliable material identification and appropriate quality controls help manufacturers maintain consistent production processes.
Industries That Depend on Chemical Raw Materials
Different industries require different combinations of chemicals.
Manufacturing and engineering: Industrial chemicals support metal treatment, equipment maintenance, surface finishing, and component production.
Construction: Resins, pigments, sealants, and selected additives are used in coatings, concrete formulations, insulation, and protective materials.
Textiles: Dyes, finishing agents, and processing chemicals support fabric coloration and material treatment.
Packaging and plastics: Polymers, stabilizers, colorants, and processing additives contribute to product formation.
Agriculture: Fertilizer ingredients and other agricultural chemical inputs support crop production and related processes.
Water and environmental management: Selected chemicals are used in treatment systems, depending on water composition and treatment objectives.
Why Supplier Quality Matters
Material quality influences manufacturing performance, consistency, and workplace safety. Differences in concentration, moisture content, contamination levels, or particle size can change how a chemical behaves during production.
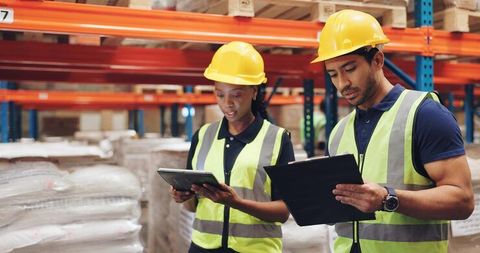
Industrial purchasers therefore examine specifications alongside supplier documentation. They may also assess batch consistency, storage practices, packaging suitability, traceability, and the supplier's ability to communicate changes in product composition.
Supplier evaluation is particularly important when a material is used in a tightly controlled production process. Substituting one chemical grade for another without technical review may affect equipment, finished products, or worker safety.
Common Procurement Challenges
Chemical procurement involves more than identifying a product name. Purchasers must consider several connected factors:
Specification matching: Confirming that the chemical composition, grade, concentration, and physical form suit the intended process.
Supply continuity: Understanding lead times, inventory availability, transport limitations, and potential disruptions.
Documentation: Checking labels, batch records, safety information, and applicable conformity documents.
Storage and transport: Confirming that containers, temperature conditions, and handling arrangements suit the material.
Traceability: Maintaining records that connect delivered batches with their source and subsequent use.
Addressing these factors helps organizations understand operational risks before materials enter production.
Recent Updates
The chemical supply sector continues to adapt to changing manufacturing requirements, environmental considerations, digital procurement systems, and supply chain uncertainty. Recent developments from 2024–2026 reflect broader efforts to improve traceability, operational visibility, chemical safety, and resource efficiency.
Digital Procurement and Supply Chain Visibility
Digital procurement platforms increasingly support supplier records, purchase planning, inventory monitoring, order documentation, and shipment tracking. These systems can help organizations compare specifications and organize purchasing information across multiple suppliers.
Digital records also make it easier to maintain batch histories and identify documentation gaps. However, software records do not independently confirm chemical purity or guarantee that delivered materials meet specifications. Physical inspection, appropriate testing, and document verification remain important.
Greater Attention to Product Traceability
Manufacturers are paying closer attention to the origin and composition of chemical inputs. Traceability can be particularly important when materials pass through several distributors before reaching the final industrial user.
Electronic certificates, standardized product identifiers, and organized batch documentation can support this process. Their usefulness depends on accurate records and suitable verification procedures.
Sustainability and Resource Efficiency
Chemical manufacturers and industrial purchasers are examining ways to reduce waste, improve material efficiency, and manage environmental impacts. Examples include process optimization, solvent recovery, recycled feedstocks where technically appropriate, and the development of chemicals with improved environmental profiles.
These approaches require careful evaluation because environmental performance depends on the material, production method, application, and disposal pathway. A product described as sustainable should still be assessed using relevant technical and environmental evidence.
Supply Chain Diversification
Industrial organizations may evaluate multiple qualified suppliers or alternative sourcing routes to reduce dependence on a single source. This approach can help identify supply risks related to transportation disruptions, changing raw material availability, and regional production constraints.
Alternative suppliers must still meet the required specifications. Changing the source of a chemical may require sample testing, production trials, revised documentation, or approval under the purchaser's internal quality procedures.
Laws or Policies
Chemical raw material suppliers operate within regulatory systems that address chemical identification, workplace protection, transportation, environmental management, and product-specific requirements. The applicable rules depend on the chemical, its concentration, the activity involved, and the jurisdictions through which it moves.
Because this article covers the global supply chain, no single regulatory framework applies to every supplier. Businesses must identify the requirements relevant to their locations, products, and intended applications.
Chemical Classification and Safety Documentation
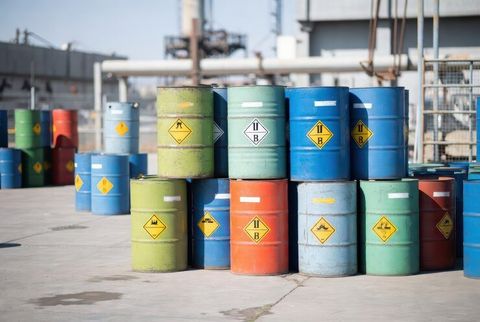
Chemical hazard communication frameworks help identify substances and communicate risks through labels and safety data sheets. These documents commonly describe hazards, handling precautions, storage conditions, first-aid measures, spill response, and other relevant safety information.
The Globally Harmonized System of Classification and Labelling of Chemicals provides an international framework for chemical classification and hazard communication. Its implementation varies by jurisdiction, so suppliers and purchasers must confirm the applicable local requirements.
Transportation and Storage Requirements
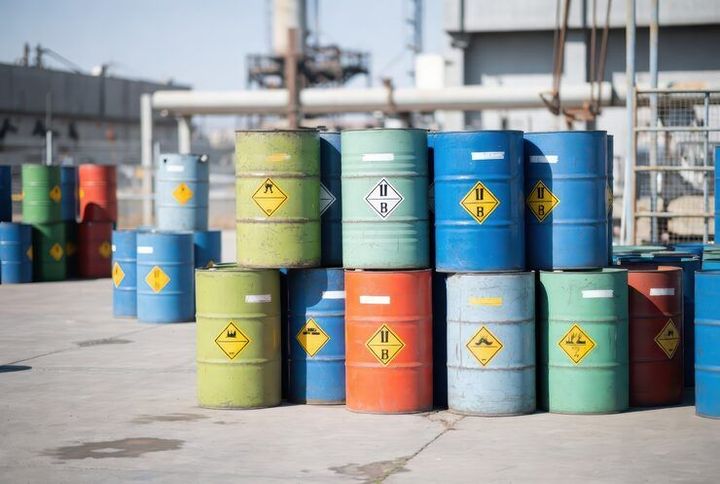
Some chemicals require specialized packaging, hazard labels, transport documentation, or temperature-controlled storage. Dangerous goods rules may apply during road, rail, sea, or air transportation, depending on the substance and its classification.
Storage arrangements may also require segregation of incompatible chemicals, spill containment, ventilation, fire protection, and controlled access. The exact precautions depend on the material's properties and the relevant workplace and environmental rules.
Environmental and Product-Specific Controls
Certain chemicals are subject to additional restrictions involving production, importation, use, emissions, waste handling, or disposal. Product categories such as agricultural inputs, food-contact materials, and chemicals used in particular industrial applications may have separate requirements.
Supplier documentation should therefore be evaluated in relation to the intended use rather than treated as universally sufficient. Compliance records, product approvals, and testing requirements may differ across markets.
Tools and Resources
Chemical procurement teams use technical documents, supplier assessment methods, inventory systems, and regulatory information to evaluate materials. The appropriate tools depend on the chemical category and the complexity of the production process.
Technical Data and Safety Documents
Two important documents are the technical data sheet and the safety data sheet. A technical data sheet describes product characteristics, specifications, performance parameters, and recommended application conditions. A safety data sheet focuses on hazards, safe handling, storage, exposure controls, and emergency procedures.
A certificate of analysis may provide batch-specific test results, including selected purity measurements, concentration values, or other specification limits. Purchasers should check whether the certificate relates to the actual delivered batch and whether its testing methods meet their requirements.
Supplier Evaluation Checklist
A consistent evaluation template helps compare chemical raw material suppliers using similar criteria.
Evaluation area | Information to review | Purpose |
|---|---|---|
Product specifications | Grade, concentration, purity, physical form | Confirm application suitability |
Quality documentation | Test results and batch certificates | Assess conformity with requirements |
Safety information | Labels and safety data sheets | Understand handling risks |
Packaging | Container type and material compatibility | Reduce leakage and contamination risks |
Supply capacity | Inventory, lead times, delivery arrangements | Assess supply continuity |
Traceability | Batch numbers and source records | Support quality investigations |
Regulatory status | Applicable permits and compliance records | Review relevant legal requirements |
The checklist can be adapted to the material and manufacturing process. Not every category requires the same tests or documents.
Procurement and Inventory Systems
Enterprise resource planning systems, inventory management software, and procurement platforms help organizations maintain supplier records, monitor stock levels, track orders, and organize purchasing approvals. These tools can also support reorder planning and documentation management.
A basic procurement worksheet may include the chemical name, internal material code, required grade, approved supplier, quantity, storage conditions, batch number, delivery status, and document review status. Keeping these fields consistent can reduce confusion when several similar chemicals are used at the same facility.
FAQs
What do chemical raw material suppliers provide?
Chemical raw material suppliers provide industrial substances such as solvents, acids, alkalis, resins, pigments, polymers, and specialty chemicals. Depending on their role, they may also coordinate packaging, transport, technical documentation, and batch traceability.
How can businesses evaluate chemical raw material suppliers?
Businesses can examine product specifications, quality records, safety documentation, traceability, packaging practices, regulatory compliance, and supply capacity. Technical testing may also be necessary when material quality directly affects manufacturing performance.
What documents should chemical suppliers provide?
Relevant documents may include technical data sheets, safety data sheets, certificates of analysis, product labels, and shipment records. The required documentation depends on the substance, application, and applicable regulations.
How does chemical raw material quality affect manufacturing?
Variations in purity, concentration, moisture, or contamination can influence processing conditions and finished-product consistency. Appropriate specifications, batch verification, and incoming quality checks help identify potential problems.
What should procurement teams consider when sourcing industrial chemicals?
Procurement teams should evaluate technical suitability, supplier reliability, documentation, packaging, storage requirements, transportation arrangements, and regulatory obligations. They should also consider supply continuity and whether any proposed material substitution requires technical approval.
Conclusion
Chemical raw material suppliers connect chemical producers with industries that depend on consistent material inputs. Product specifications, quality documentation, safe handling, traceability, and regulatory compliance are important elements of the supply chain. Digital procurement tools and sustainability initiatives are influencing how businesses manage chemical sourcing and inventory. The appropriate supplier evaluation process depends on the chemical's properties, intended application, and applicable requirements.